 Central Steel
Central Steel
Hot-rolled seamless steel pipe defects are mainly caused by raw material quality, billet heating, piercing and rolling parameters, equipment condition, and improper process control. Common defects include surface scratches, pits, cracks, folds, seams, hairline defects, lamination, dimensional deviations, and straightness problems. Effective billet inspection, accurate temperature control, optimized rolling parameters, regular equipment maintenance, and final inspection can significantly reduce these defects and improve the quality and reliability of hot-rolled seamless steel pipes.
This article explains the most common defects in hot-rolled seamless steel pipes, their causes, and the main measures used to prevent them.
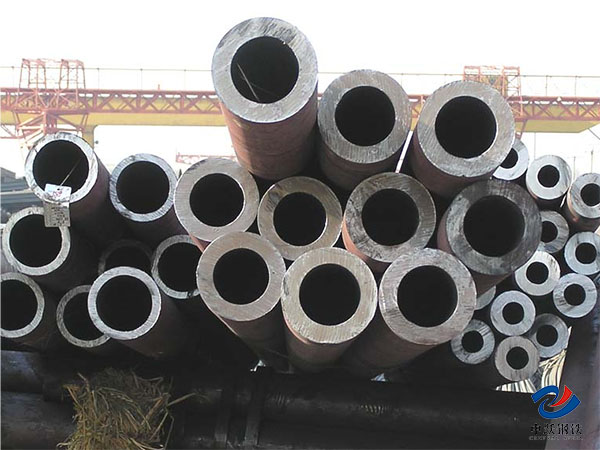
Common Defects in Hot-Rolled Seamless Steel Pipes
The following table summarizes the major defects, their typical appearance, main causes, and recommended prevention measures.
|
Defect |
Typical Appearance |
Main Causes |
Prevention |
|
Surface scratches |
Linear marks or scratches on the inner or outer surface |
Billet surface defects, oxide scale, friction with equipment |
Improve billet surface quality and maintain rolling equipment |
|
Pits |
Small or localized depressions on the pipe surface |
Oxide scale, inclusions, surface contamination, or equipment damage |
Clean billets and inspect equipment regularly |
|
Cracks |
Straight, longitudinal, transverse, or irregular cracks |
Poor billet quality, improper heating, excessive deformation, or stress concentration |
Inspect billets and optimize heating and rolling parameters |
|
Hairline defects |
Fine continuous or discontinuous lines on the surface |
Subsurface inclusions, cracks, scale, or improper piercing/rolling |
Improve billet quality and control piercing and rolling conditions |
|
Inner folds |
Folded or irregular defects on the inner surface |
Billet defects, improper piercing, uneven deformation, or incorrect rolling parameters |
Optimize piercing and rolling parameters |
|
Outer folds / seams |
Longitudinal or spiral surface defects |
Billet surface defects, excessive deformation, or improper mill adjustment |
Improve billet inspection and mill adjustment |
|
Lamination |
Layer-like or planar separation on the surface or inside the pipe |
Inclusions, porosity, or other billet-related defects |
Strengthen billet quality control and use appropriate NDT |
|
Dimensional deviation |
OD, ID, or wall thickness outside the specified tolerance |
Incorrect sizing parameters, worn rolls, or unstable rolling conditions |
Calibrate equipment and monitor dimensions during production |
|
Poor straightness |
Pipe bends or deviates from the specified straightness |
Uneven cooling, improper straightening, or dimensional variation |
Control cooling and optimize straightening |
|
Uneven wall thickness |
Wall thickness varies around or along the pipe |
Off-center piercing, uneven deformation, or improper sizing |
Control piercing alignment and optimize rolling parameters |
Frequently Asked Questions About Hot-Rolled Seamless Steel Pipe Defects
1. What are the most common defects in hot-rolled seamless steel pipes?
The most common defects include surface scratches, pits, cracks, hairline defects, folds, seams, lamination, uneven wall thickness, dimensional deviations, and poor straightness. Most defects are related to billet quality, heating, piercing, rolling, equipment condition, or process control.
2. What causes cracks in hot-rolled seamless steel pipes?
Cracks can be caused by poor billet quality, subsurface cracks or inclusions, improper heating, excessive deformation, incorrect piercing conditions, or local stress concentration during rolling.
3. What causes folding defects in seamless steel pipes?
Folding defects are commonly associated with billet surface or subsurface defects, inclusions, uneven heating, improper piercing, excessive deformation, and incorrect rolling or equipment parameters.
4. What causes surface scratches on hot-rolled seamless steel pipes?
Surface scratches can result from billet surface defects, residual oxide scale, foreign particles, or friction between the pipe and damaged or contaminated production equipment.
In summary, by improving raw material quality, optimizing process parameters and strengthening equipment management, these defects can be effectively prevented and reduced, thereby improving product quality and safety.
Read more : What is a seamless steel pipe?
 Language
 English
 Español
 بالعربية
 sales@central-steels.com
 0086-731-8865-5017